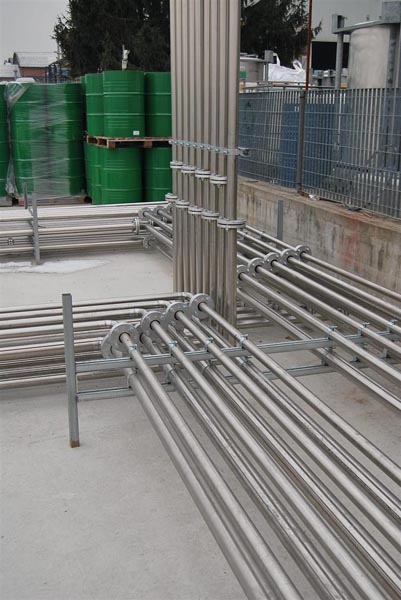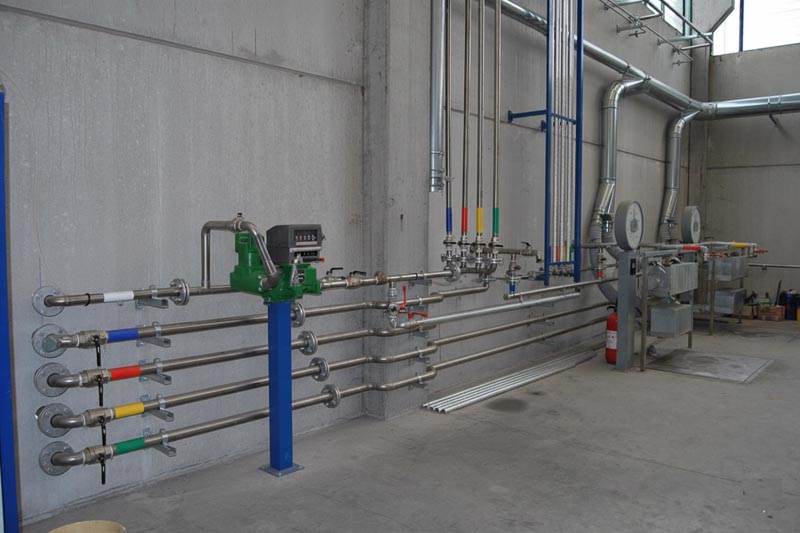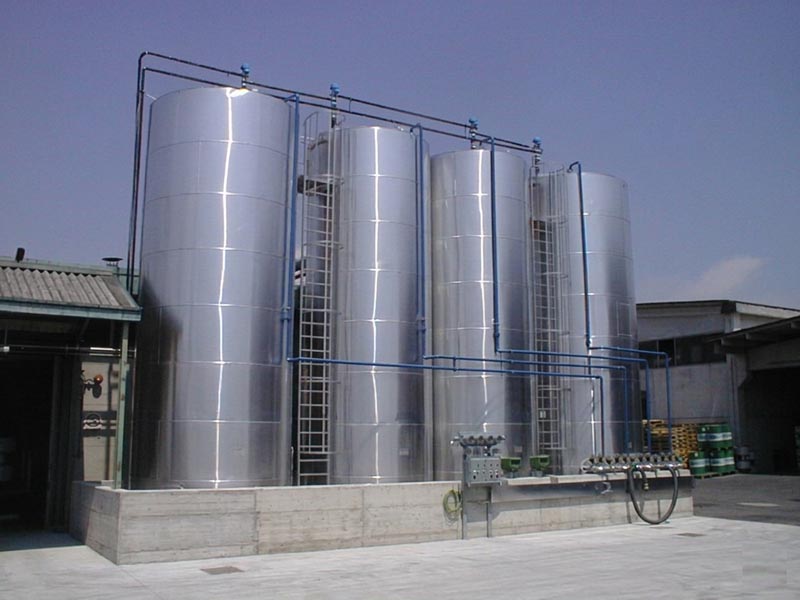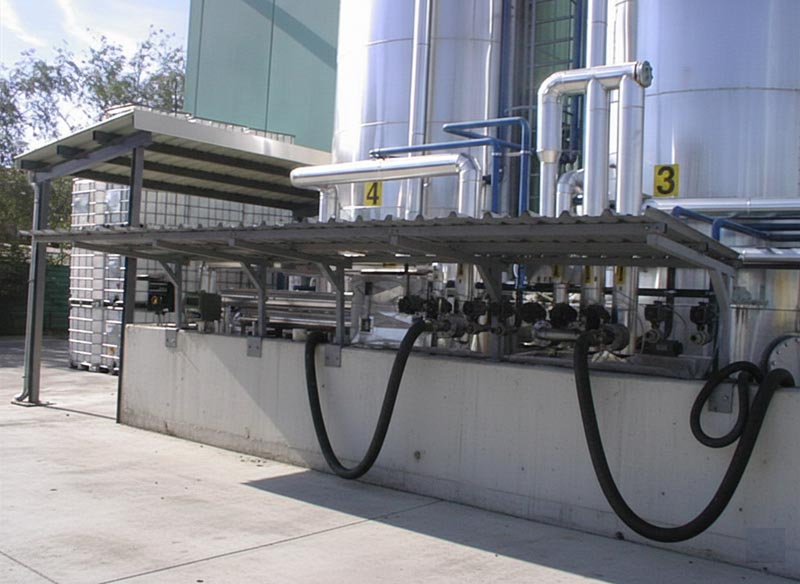
Solvent Processing Equipment
Our company specializes in the design, engineering, and installation of state-of-the-art bulk solvent storage systems, available in both above-ground (AST) and underground (UST) configurations. Designed to meet the highest safety and environmental standards, these systems offer reliable, comprehensive solutions for managing highly flammable and volatile industrial solvents.
Fully compliant with the ATEX Directive for explosive atmospheres, our systems are specifically designed to safely store and handle a wide range of hazardous substances, including:
• Hydrocarbons and alkanes: n-pentane, n-hexane, cyclohexane
• Aromatic compounds: Toluene, Xylene
• Ketones: Acetone, Methyl ethyl ketone (MEK)
• Esters and alcohols: Ethyl acetate, Isopropyl alcohol (IPA)
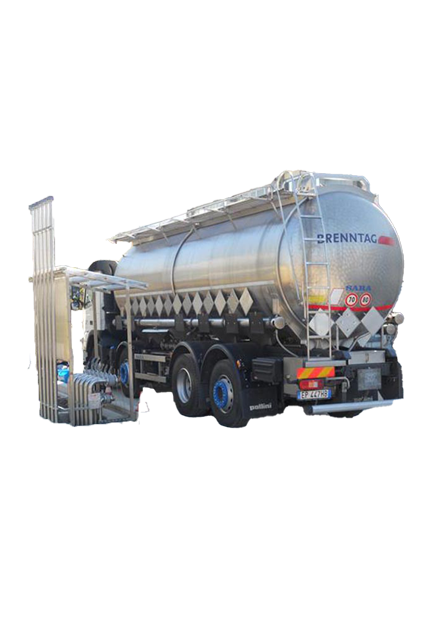
- ATEX-compliant design: all electrical components, instrumentation, pumps, and grounding systems are rigorously certified for ATEX hazardous areas—Zone 0/1 (internal) and Zone 1/2 (external)—to prevent ignition sources.
- Tank configurations:
- Above-ground storage tanks (AST): equipped with integrated containment bunds (containment walls) or a double-walled structure to ensure complete spill containment.
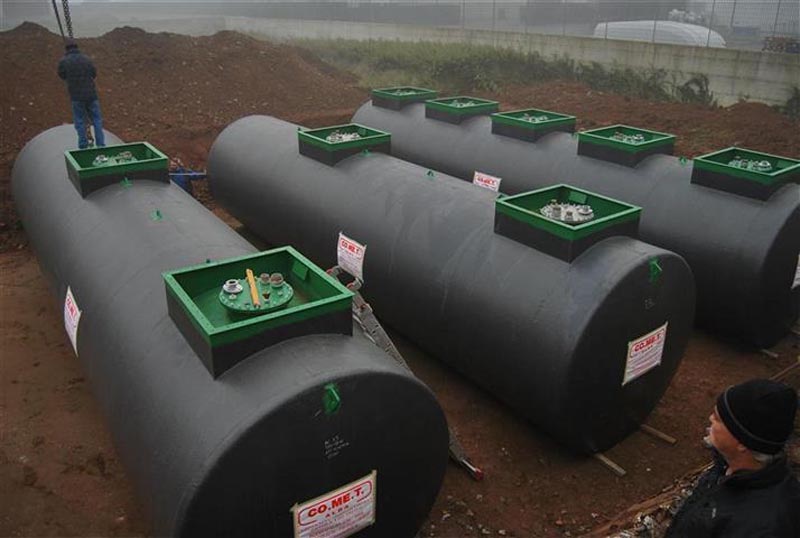
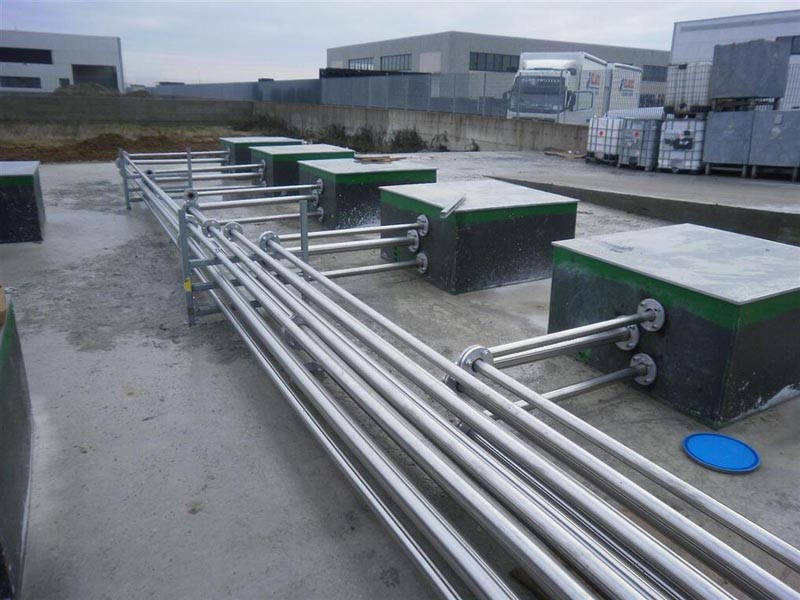
- Underground storage tanks (UST): double-walled structure with continuous interstitial leak detection monitoring (vacuum or liquid-based).
- Vapor management and nitrogen blanketing: to prevent explosive atmospheres and product degradation, the tanks are equipped with automated nitrogen ($N_2$) inerting systems, pressure/vacuum relief valves (PVRV), and flame arresters.
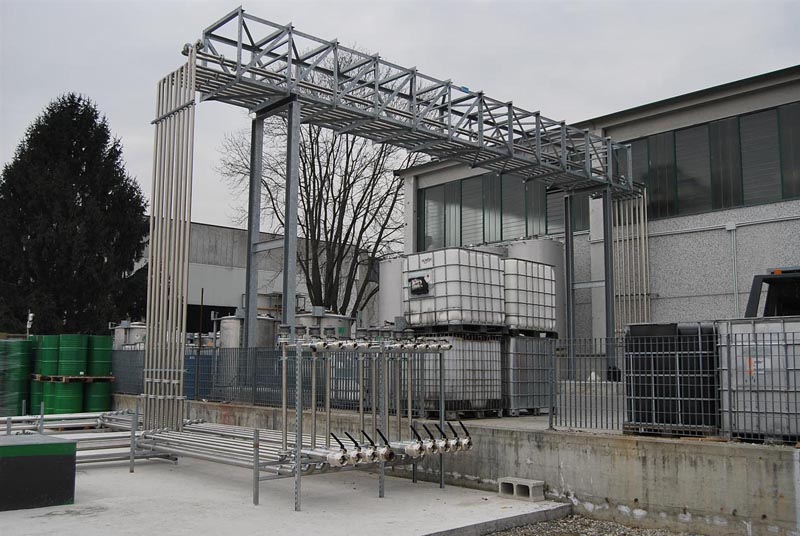
- Advanced instrumentation: continuous radar level measurement, overfill prevention switches, automatic shut-off valves (ESD), and dedicated gas detection circuits integrated into the main PLC control panel.
Discover the photo gallery: